Bearing Retention in Stamped Steel Housings: Tolerance Ring vs. Press Fit
Progressive stamping is a cost-effective and repeatable forming process, well suited to producing things like motor housings, enclosures, and structural brackets at volume. The trouble starts when that stamped housing also has to serve as a precision bearing retention mount.
Bearing fits are typically designed with the interference on the shaft side and a slip fit in the housing. In a stamped housing, that assumption gets complicated. As-stamped bore tolerance typically runs around .005″, and the bore is often out-of-round as well. Depending on where a given part falls within that range, the same nominal design can end up as an unintentionally heavy press at one end or a loose, spinning fit at the other. And an out-of-round bore can distort the bearing’s outer ring in the process.
The straightforward fix is to machine the bore after stamping. That works, but it adds a secondary operation to a production line designed to avoid one. At volume, the cost adds up quickly, and it reintroduces the lead time and tooling overhead that progressive stamping was intended to eliminate.
A tolerance ring solves this problem without machining. It accommodates as-stamped bore variation and delivers consistent radial bearing retention force across the full manufacturing tolerance range.
How a Tolerance Ring Works for Bearing Retention in a Stamped Housing
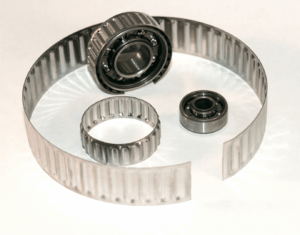
A tolerance ring is a thin-walled metal ring with formed corrugations (wave crests) that deflect elastically under compression to generate controlled radial bearing retention force. Installed between a bearing outer race and a housing bore, the corrugations compress against the outer race, holding the bearing in position without a machined interference.
The key mechanical property is the relationship between ring spring stiffness and housing stiffness. For this mechanism to work as intended, the ring’s spring stiffness must be lower than the stiffness of the surrounding housing. When bore diameter varies across the manufacturing tolerance range, the ring compresses or expands slightly rather than transmitting that variation as a proportional change in retention force. The ring absorbs bore variation; a rigid interference fit transmits it.
Because the ring operates within its elastic range across the full bore tolerance band, the radial force it generates scales gradually with bore dimension. At maximum bore clearance, the ring is less compressed but still produces sufficient retention force. At minimum bore dimension, the ring is more compressed and generates higher radial force, but here the ring geometry matters. The corrugation geometry is specified so that even at maximum compression, the radial force applied to the bearing outer race does not reduce bearing internal clearance below its operating specification.
This is the critical distinction from a press fit. An interference fit scaled to retain the bearing at maximum bore clearance will, at minimum bore dimension, apply a preload that can compress internal clearance below the bearing’s design limit, generating heat, noise, and shortened fatigue life. A properly sized tolerance ring bounds the maximum radial force through its spring rate, providing a self-adjusting fit across the full bore tolerance range that a fixed interference cannot replicate.
For a detailed look at radial force behavior, ring selection criteria, and load considerations, see our resource on tolerance rings in ball bearing applications.
AN-Style Ring Geometry for Outer Race Retention
Tolerance ring geometry varies by application. For a stamped housing bearing mount where the objective is to secure the bearing outer race to the housing bore, the AN configuration is the standard choice.
AN-style rings have their corrugation waves oriented inward, toward the bore centerline. The wave crests contact the bearing outer race; the unformed cylindrical band of the ring seats against the housing bore wall. This places the elastic element at the outer race interface, applying retention force there while the ring body maintains stable contact with the housing.
The AN style is also compatible with automated assembly. Because the ring seats with a controlled, repeatable insertion force rather than a precisely calibrated interference, it can be incorporated into automated assembly sequences without the tooling complexity required for hydraulic press operations.
Ball Bearing Retention Without Machining: What This Looks Like in Production
When the ring is correctly specified for the application (geometry matched to the bore tolerance range and retention load requirement) the production-level outcomes typically include:
No secondary bore finishing
The housing moves from the stamping press directly into the assembly sequence. The ring accommodates as-stamped bore dimensions; there is no bore machining step to add to the process flow or tooling budget.
Consistent retention force across the full bore tolerance range
Because ring radial force scales elastically with bore dimension, retention stays within specification at both ends of the manufacturing tolerance band. There is no need to sort parts or maintain a tighter bore tolerance at the stamping operation.
Bearing internal clearance preserved at minimum bore dimension
The ring’s spring rate limits maximum radial force even when the bore runs small. The bearing operates with the internal clearance it was designed for.
Automated assembly compatibility
Ring installation does not require a press force calibrated to a specific interference. The controlled insertion load is consistent with automated tooling on a production line.
Reduced tolerance demands on the stamping operation
Without downstream pressure to hold bore dimensions tighter than the stamping process is designed for, die replacement schedules can follow actual wear rather than compensating for process variation.
Designing for Bearing Retention from the Start
The conflict between press fit requirements and stamped bore variation is easiest to address during initial design. Once the stamping tool is built, the housing geometry is fixed and the bearing is specified. From there, retrofit options narrow to three paths: adding a machining operation, accepting reduced retention reliability at the loose end of the bore range, or redesigning the retention interface for a tolerance ring. All three carry more cost and disruption than designing for the ring from the start.
If the housing forming process is stamping and the housing must carry a ball bearing, the bearing retention method should be evaluated alongside the housing design. A tolerance ring adds one component to the bore assembly and removes a secondary machining operation from the process plan. The ring geometry is specified to the bore tolerance range and the required retention load; from there, retention performance is consistent across the production run without additional process controls.
Solving the Bearing Retention Problem in Stamped Housings
Stamped steel housings introduce bore variation that exceeds the tolerance window a standard press fit requires. Machining the bore after stamping resolves the dimensional problem but adds process cost and complexity. A tolerance ring addresses the problem at the interface: Its elastic spring rate absorbs bore variation and delivers consistent radial retention force across the full as-stamped tolerance range, while bounding maximum radial force at minimum bore dimension to protect bearing internal clearance.
If you are working through a bearing retention problem in a stamped housing, our engineers can evaluate ring geometry and radial force requirements for your specific bore tolerance and load conditions. Contact our engineering team or review our bearing retention solutions.
Frequently Asked Questions
Can you use a press fit in a stamped steel housing?
Using a press fit for bearing retention in a stamped steel housing is possible, but unreliable at production volume, and a slip fit doesn’t solve the problem either. A reliable press fit for a precision ball bearing requires the housing bore to be held within a narrow window, often as small as a few ten-thousandths of an inch. Progressive stamping introduces bore variation that is wider than this tolerance window – an inherent result of die wear, material springback, and the forming process, not a quality failure. The same bore variation that makes a press fit unreliable can also leave a slip fit loose enough to let the bearing spin in the housing, and bore out-of-roundness can affect either fit type. To make a press fit work in a stamped housing, the bore would need to be machined after stamping, adding a secondary operation that offsets much of the cost advantage of the stamping process. A tolerance ring is designed for this condition: It accommodates as-stamped bore variation and delivers consistent radial retention force without a post-stamp machining step.
How does a tolerance ring preserve bearing internal clearance?
A tolerance ring preserves bearing internal clearance because its spring rate limits the maximum radial force it applies, even when the housing bore is at minimum dimension. In a rigid interference fit, a bore that runs small increases the interference proportionally. Depending on the degree of preload and the application, this can increase operating temperature, generate noise, and accelerate fatigue damage. A tolerance ring operates within a defined elastic range. At minimum bore dimension, the ring compresses further and generates higher radial force, but that force is bounded by the ring’s spring stiffness. When the ring is correctly specified for the application, the geometry ensures that even at maximum compression, the radial force applied to the outer race does not reduce internal clearance below the bearing’s operating specification.
What causes bore variation in a stamped steel housing?
Bore variation in progressive stamping is driven by three factors: die wear over production runs, material springback after the forming stroke, and the inherent mechanics of the forming operation. This variation is a process characteristic, not a defect, but it directly conflicts with the narrow tolerance window a standard press-fit bearing retention requires.
What is an AN-style tolerance ring?
An AN-style tolerance ring is a ring configuration in which the corrugation wave crests face inward, toward the bore centerline. When installed, the wave crests contact the bearing outer race and the unformed cylindrical band of the ring seats against the housing bore wall. This geometry is appropriate for applications where the bearing outer race is being retained within a housing bore (such as a stamped housing bearing mount) because it applies retention force directly to the outer race while maintaining stable contact with the housing. The AN style is also compatible with automated assembly processes, as its installation load is consistent and repeatable rather than dependent on a precisely calibrated interference.
When should the bearing retention method be specified, at design or during production?
Bearing retention method is best specified during initial design, before the stamping tool is built. Once the tool and housing geometry are fixed, retrofit options are limited to adding a machining operation, accepting reduced retention reliability, or redesigning the bore interface, all of which carry more cost than designing for a tolerance ring from the outset.